Introduction to Chocolate Boxes
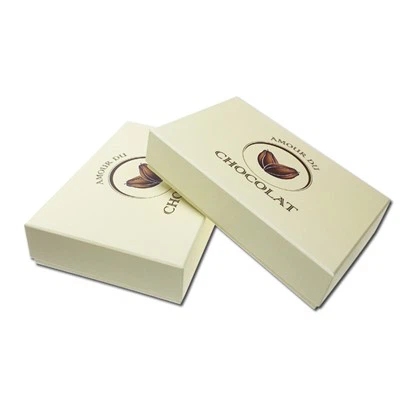
Chocolate boxes are not merely containers; they are an integral part of the chocolate - consuming experience. They serve multiple purposes, from protecting the delicate chocolates inside to enhancing their visual appeal. A well - designed chocolate box can communicate the brand's identity, evoke emotions, and even tell a story. It can range from simple, elegant designs for high - end chocolates to more colorful and whimsical ones for mass - market products. The choice of materials, such as cardboard, wood, or metal, and the printing techniques used, like embossing, foiling, or digital printing, all contribute to the overall quality and attractiveness of the chocolate box. In the highly competitive chocolate market, a factory that can produce innovative, high - quality chocolate boxes has a significant edge.
1. Humen Hengyue Paper Products Factory
Humen Hengyue Paper Products Factory is a well - established player in the field of chocolate box manufacturing. Based in China, the factory has a long - standing reputation for its commitment to quality and innovation.
Company Introduction
The factory was founded several decades ago and has since grown into a large - scale operation. It has a team of experienced designers who are constantly researching the latest trends in packaging design. They understand that chocolate boxes need to not only look good but also be functional. For example, they design boxes with proper partitions to keep chocolates separated and prevent them from getting damaged during transportation.
The factory uses state - of - the - art production equipment. It has advanced printing machines that can achieve high - resolution and vivid colors on the boxes. The quality control system is strict, ensuring that every box that leaves the factory meets the highest standards. They also offer customization services, allowing chocolate brands to have unique boxes tailored to their specific needs. Whether it's a small - batch order for a boutique chocolate shop or a large - scale production for a well - known brand, Humen Hengyue Paper Products Factory can handle it efficiently.
Features and Advantages in Chocolate Box Production
- Customization: The factory offers a high degree of customization. Chocolate brands can choose from a wide range of materials, including different grades of cardboard, and can have their logos, brand stories, and unique designs printed on the boxes. They can also select from various finishing options such as matte or gloss coatings, embossing, and debossing.
- Quality Assurance: With a strict quality control process in place, the factory ensures that each chocolate box is free from defects. They conduct multiple inspections during the production process, from the raw material stage to the final product. This attention to detail guarantees that the chocolate boxes can withstand the rigors of transportation and storage.
- Cost - effectiveness: Despite offering high - quality products, Humen Hengyue Paper Products Factory is able to keep its costs competitive. This is due to its efficient production processes and economies of scale. It can provide chocolate brands with cost - effective packaging solutions without compromising on quality.
- Sustainable Practices: The factory is increasingly focused on sustainable production. It uses eco - friendly materials whenever possible and has implemented recycling programs in its production facilities. This is in line with the growing consumer demand for sustainable packaging in the chocolate industry.
Website: https://www.hengyuanprinting.com/
2. DS Smith Packaging
Company Introduction
DS Smith is a leading global packaging company with a significant presence in the chocolate box manufacturing sector. Headquartered in the UK, the company has a vast network of production facilities across Europe, North America, and Asia. It has a long history dating back over 100 years and has continuously evolved to meet the changing needs of the packaging industry.
DS Smith has a strong focus on innovation. It invests heavily in research and development to come up with new packaging solutions. For chocolate boxes, this means exploring new materials and designs that can enhance the shelf - life of chocolates, reduce environmental impact, and improve the overall consumer experience. The company also works closely with chocolate brands to understand their marketing strategies and develop packaging that aligns with their brand image.
Features and Advantages in Chocolate Box Production
- Innovative Designs: DS Smith's design team is constantly pushing the boundaries of traditional chocolate box design. They create unique shapes and structures that not only stand out on the shelf but also provide practical benefits. For example, they have developed boxes with easy - open features and re - sealable options, which are very popular among consumers.
- Supply Chain Efficiency: With its global network of facilities, DS Smith can ensure a reliable and efficient supply of chocolate boxes. It can quickly respond to changes in demand from chocolate brands and deliver products in a timely manner. This is crucial for the chocolate industry, which often has seasonal peaks in demand.
- Sustainable Packaging Solutions: DS Smith is at the forefront of sustainable packaging. It uses a high percentage of recycled materials in its chocolate boxes and is committed to reducing its carbon footprint. The company also helps chocolate brands communicate their sustainability efforts through the packaging, which is becoming increasingly important to consumers.
- Technical Expertise: The company has a deep understanding of the technical aspects of chocolate box production. It can optimize the design of boxes to ensure proper ventilation, which is important for maintaining the quality of chocolates. It also has expertise in printing techniques, allowing for high - quality graphics and branding on the boxes.
3. WestRock Company
Company Introduction
WestRock is a major player in the packaging industry, with a significant share in the chocolate box market. Based in the United States, the company has a diverse portfolio of packaging products and services. It has a large number of manufacturing plants across North America and other regions, which gives it the capacity to produce chocolate boxes in large volumes.
WestRock has a strong customer - centric approach. It works closely with chocolate manufacturers to understand their specific requirements and challenges. For example, it takes into account factors such as the type of chocolates being packaged (e.g., truffles, bars), the target market, and the distribution channels when designing chocolate boxes. The company also has a team of experts in areas such as food safety and packaging regulations, ensuring that its chocolate boxes meet all the necessary standards.
Features and Advantages in Chocolate Box Production
- Large - Scale Production: WestRock's extensive manufacturing facilities allow it to handle large - scale chocolate box orders. This is beneficial for big chocolate brands that require a consistent supply of high - quality boxes. The company can also ramp up production quickly during peak seasons, such as Christmas and Valentine's Day.
- Food - Grade Packaging: Given the nature of the product being packaged (chocolates), WestRock places a high emphasis on food - grade packaging. It uses materials that are safe for direct contact with food and has strict quality control measures in place to ensure compliance with food safety regulations.
- Market Insights: The company has a wealth of market insights, which it shares with its chocolate brand customers. It can provide data on consumer trends, such as the popularity of certain packaging styles or colors, and help brands make informed decisions about their chocolate box designs.
- Integrated Solutions: WestRock offers integrated packaging solutions. In addition to manufacturing chocolate boxes, it can also provide services such as logistics, inventory management, and point - of - sale displays. This one - stop - shop approach is very convenient for chocolate brands.
4. Smurfit Kappa Group
Company Introduction
Smurfit Kappa is an international packaging company with a strong foothold in the chocolate box industry. Headquartered in Ireland, the company has operations in over 30 countries. It has a rich heritage in packaging, with a history spanning more than 100 years.
The company is known for its customer - focused approach. It has dedicated account managers for each chocolate brand client, who work closely with the brand's marketing and product development teams. This ensures that the chocolate boxes are designed and produced to meet the brand's specific marketing goals and product requirements. Smurfit Kappa also has a strong commitment to sustainability, which is reflected in its chocolate box production.
Features and Advantages in Chocolate Box Production
- Global Reach: With its widespread operations, Smurfit Kappa can serve chocolate brands on a global scale. It can produce and distribute chocolate boxes to different markets around the world, which is a significant advantage for international chocolate brands.
- Sustainable Packaging Leadership: The company is a leader in sustainable packaging. It uses 100% recyclable materials in its chocolate boxes and has set ambitious targets for reducing its environmental impact. This is not only good for the planet but also helps chocolate brands meet the growing consumer demand for sustainable products.
- Design Flexibility: Smurfit Kappa offers a high degree of design flexibility. It can create chocolate boxes in a wide range of sizes, shapes, and colors. Whether it's a classic, elegant box for a luxury chocolate brand or a fun, modern design for a new - age chocolate product, the company can deliver.
- Value - Added Services: In addition to manufacturing chocolate boxes, Smurfit Kappa provides value - added services such as packaging testing and optimization. It can test the durability of boxes during transportation and storage and make adjustments to the design to improve performance.
5. Amcor Limited
Company Introduction
Amcor is a global leader in packaging solutions, with a significant presence in the chocolate box market. Based in Australia, the company has a diverse product portfolio that includes flexible and rigid packaging. It has a strong focus on innovation and has been at the forefront of developing new packaging technologies.
For chocolate box production, Amcor works closely with chocolate manufacturers to understand the unique properties of their chocolates. For example, some chocolates are more sensitive to temperature and humidity, and Amcor can design boxes that provide the appropriate level of protection. The company also has a global network of research and development centers, which allows it to stay ahead of the curve in terms of packaging trends.
Features and Advantages in Chocolate Box Production
- Advanced Packaging Technologies: Amcor is known for its use of advanced packaging technologies. It can incorporate features such as barrier coatings in chocolate boxes to protect chocolates from oxygen, moisture, and light. This helps to extend the shelf - life of chocolates and maintain their quality.
- Global R & D Network: The company's global research and development network enables it to quickly adapt to new market trends and consumer demands. It can develop new chocolate box designs and materials that are in line with the latest industry standards and consumer preferences.
- Customized Solutions: Amcor offers highly customized chocolate box solutions. It can work with chocolate brands to create packaging that reflects their brand personality and marketing message. This includes everything from the choice of materials to the printing and finishing options.
- Regulatory Compliance: Amcor has a deep understanding of the regulatory requirements in different markets. It ensures that all its chocolate boxes comply with local and international regulations, which is crucial for chocolate brands operating in multiple countries.
6. Sonoco Products Company
Company Introduction
Sonoco is a well - established packaging company with a long history in the chocolate box manufacturing business. Headquartered in the United States, the company has a wide range of packaging products and services. It has a strong focus on customer service and has built long - term relationships with many chocolate brands.
Sonoco's design team has a good understanding of the chocolate industry. They know what kind of packaging can attract consumers and enhance the brand image of chocolate products. The company also invests in new technologies to improve the efficiency and quality of its chocolate box production.
Features and Advantages in Chocolate Box Production
- Customer - Centric Service: Sonoco places a high priority on customer service. It assigns dedicated account managers to each chocolate brand client, who are available to answer questions and address concerns throughout the production process. This personalized service ensures that the chocolate boxes meet the exact requirements of the brand.
- Advanced Manufacturing Processes: The company uses advanced manufacturing processes to produce high - quality chocolate boxes. It has automated production lines that can ensure consistent quality and high production volumes. Sonoco also invests in new equipment and technologies to improve the precision and speed of its production.
- Brand - Building Packaging: Sonoco's design team can create chocolate boxes that are not only functional but also help to build the brand. They use innovative printing techniques and design elements to make the boxes stand out on the shelf and communicate the brand's story to consumers.
- Sustainable Initiatives: Sonoco is committed to sustainable packaging. It uses recycled materials in its chocolate boxes and has implemented energy - saving measures in its production facilities. This helps chocolate brands meet their sustainability goals and appeal to environmentally - conscious consumers.
7. Huhtamäki Oyj
Company Introduction
Huhtamäki is a leading global packaging company with a significant presence in the chocolate box market. Based in Finland, the company has a long - standing reputation for high - quality packaging solutions. It has a wide range of production facilities across Europe, Asia, and the Americas.
The company has a strong focus on consumer trends. It conducts extensive market research to understand what consumers are looking for in chocolate packaging. This knowledge is then used to develop innovative chocolate box designs that can attract consumers and drive sales. Huhtamäki also works closely with chocolate brands to ensure that the packaging aligns with their brand values.
Features and Advantages in Chocolate Box Production
- Consumer - Driven Design: Huhtamäki's design approach is driven by consumer insights. It creates chocolate boxes that are visually appealing and easy to use. For example, it has developed boxes with ergonomic shapes and user - friendly opening mechanisms, which enhance the consumer experience.
- International Production Network: The company's international production network allows it to serve chocolate brands in different regions efficiently. It can produce chocolate boxes locally, which reduces transportation costs and lead times. This is especially important for chocolate brands that operate in multiple countries.
- Quality and Safety Standards: Huhtamäki adheres to strict quality and safety standards in its chocolate box production. It uses high - quality materials and has a comprehensive quality control system in place. This ensures that the boxes are safe for chocolates and meet the regulatory requirements of different markets.
- Sustainable Development Goals: The company is committed to achieving its sustainable development goals. It aims to increase the use of renewable materials in its chocolate boxes and reduce its environmental impact. This is in line with the growing consumer demand for sustainable packaging in the chocolate industry.
8. Constantia Flexibles Group GmbH
Company Introduction
Constantia Flexibles is a leading provider of flexible packaging solutions, with a growing presence in the chocolate box market. Headquartered in Austria, the company has a global network of production facilities. It has a strong focus on innovation and has been developing new flexible packaging solutions for chocolates.
The company works closely with chocolate manufacturers to understand their specific needs. For example, some chocolates are sold in single - serve portions, and Constantia Flexibles can design flexible chocolate boxes that are convenient for on - the - go consumption. The company also has a team of experts in packaging technology, who can provide technical support to chocolate brands.
Features and Advantages in Chocolate Box Production
- Flexible Packaging Expertise: Constantia Flexibles' core strength lies in its flexible packaging expertise. It can create chocolate boxes with unique shapes and sizes using flexible materials. This allows for more creative and space - efficient packaging designs.
- Barrier Properties: The company can incorporate excellent barrier properties into its flexible chocolate boxes. This helps to protect chocolates from external factors such as oxygen, moisture, and light, which can affect their quality. The barrier properties can be customized according to the specific requirements of the chocolates.
- Customization and Branding: Constantia Flexibles offers a high degree of customization for chocolate boxes. It can print high - quality graphics and branding on the flexible materials, allowing chocolate brands to create a strong brand identity. The company also offers different finishing options to enhance the visual appeal of the boxes.
- Technical Support: The company provides comprehensive technical support to chocolate brands. It can assist with packaging design, material selection, and production optimization. This ensures that the chocolate boxes are of the highest quality and meet the brand's expectations.
9. Uflex Limited
Company Introduction
Uflex is an Indian multinational packaging company with a significant share in the chocolate box market. It has a diverse product portfolio that includes flexible and rigid packaging solutions. The company has a large - scale production facility in India and has expanded its operations globally.
Uflex has a strong focus on research and development. It invests in new technologies and materials to improve the quality and performance of its chocolate boxes. The company also has a team of designers who are well - versed in the latest packaging trends and can create unique designs for chocolate brands.
Features and Advantages in Chocolate Box Production
- Cost - Competitive Production: Uflex is able to offer cost - competitive chocolate box production. This is due to its efficient production processes and access to cost - effective raw materials in India. It can provide chocolate brands with high - quality packaging at a lower cost compared to some international competitors.
- Diverse Product Range: The company offers a diverse range of chocolate box options, including flexible pouches, rigid boxes, and hybrid packaging solutions. This allows chocolate brands to choose the type of packaging that best suits their products and marketing strategies.
- In - house R & D: Uflex's in - house research and development department enables it to develop new packaging solutions. For example, it has developed innovative coatings for chocolate boxes that can improve their moisture - resistance and durability.
- Global Reach: Despite being based in India, Uflex has a global reach. It can export chocolate boxes to different countries and has established partnerships with chocolate brands around the world.
10. Ardagh Group S.A.
Company Introduction
Ardagh is a global packaging company with a significant presence in the chocolate box market. Headquartered in Luxembourg, the company has a wide range of packaging products, including glass, metal, and plastic packaging. It has a strong focus on sustainability and has been working towards reducing its environmental impact.
For chocolate box production, Ardagh offers a variety of options. It can produce high - end glass chocolate boxes for luxury chocolate brands, which provide a premium look and feel. The company also has expertise in metal and plastic packaging, which can be used for different types of chocolate products.
Features and Advantages in Chocolate Box Production
- Diverse Packaging Materials: Ardagh's ability to work with different packaging materials gives chocolate brands more options. They can choose between glass, metal, or plastic boxes depending on their brand image, product requirements, and target market.
- Sustainable Packaging Initiatives: The company is committed to sustainable packaging. It uses recycled materials in its chocolate boxes and has implemented energy - efficient production processes. This helps chocolate brands meet the growing consumer demand for sustainable products.
- Design and Engineering Expertise: Ardagh has a team of design and engineering experts who can create innovative chocolate box designs. They can optimize the design of boxes for functionality, aesthetics, and cost - effectiveness. For example, they can design glass boxes with unique shapes that are both visually appealing and practical.
- Global Manufacturing Network: With its global manufacturing network, Ardagh can serve chocolate brands in different regions. It can ensure a reliable supply of chocolate boxes and can quickly respond to changes in demand.
Conclusion
The top 10 chocolate box factories in the world in 2025 represent a diverse range of companies with unique strengths and capabilities. From the customization and cost - effectiveness of Humen Hengyue Paper Products Factory to the global reach and sustainable leadership of DS Smith, each factory brings something valuable to the table.
These factories are not only focused on producing high - quality chocolate boxes but also on meeting the evolving needs of the chocolate industry. They are investing in innovation, whether it's through new materials, designs, or production technologies. Sustainability is also a key focus for many of these factories, as consumers are increasingly demanding environmentally friendly packaging.
Chocolate brands have a wide range of options when it comes to choosing a chocolate box factory. They can select a factory based on their specific requirements, such as budget, design preferences, and sustainability goals. Overall, the competition among these top factories is driving the continuous improvement of chocolate box production, which is beneficial for both chocolate brands and consumers.